Liberal Forum
Archive
‹
Political Chat Rooms
‹
No Holds Barred Political Forum
‹
What jobs did you have as a teen?
What jobs did you have as a teen?
By murdock
17 Jun 2025 3:45 pm in No Holds Barred Political Forum
20 Jun 2025 7:29 am

Doubtful...probably done in some Japanese sweatshop...*GHETTOBLASTER » 20 Jun 2025, 7:04 am » wrote: ↑ I wonder if Ford heats the housing and chills the bushings for more of a drop in fit...?

 JuCo 5 percenter...72
“Show me the man and I’ll find you the crime” ~ LAVRENTIY BERIA
"Try to get past your passionate ignorance and learn to accept what actually happened." ~ brown's unheeded words of wisdom
 If gender is not sex, why should a gender claim change what sex you shower with?
"Libruls are often fascists on vacation..."

20 Jun 2025 7:37 am
I love Casey's bluing paste. I've gotten some excellent finishes using that stuff, of course the polishing is the key. Corrosion resistance of chemical bluing is actually much better than reported on gun forums by "purists" who only trust hot bluing/salts process.*GHETTOBLASTER » 19 Jun 2025, 11:15 am » wrote: ↑ Wear and corrosion resistance is part of the deal too.
Now you need to become a DIY Cadmium Plater and Metallurgist too.
Well, you're way ahead of me. At least you can give it a go. Really, the most difficult thing about the stamped parts is bending them correctly. Rog and I have discussed metal bending. I got one of those small metal benders just to play around with it and see what it is capable of doing. So far, I'm not particularly impressed. It's not precise enough. And, I can't find a bender that is designed to make precision bends. I just don't think one exists.If I had to dissect and clone that parts group in your photo.....then get all of the bugs worked out of the reproduction part during the operational testing phase...iy could take a month if everything went well on the first try...!
I've got a similar mechanism to try to reproduce on my own ....an early Jeep Cherokee door latch assy that is no longer easy to find.
20 Jun 2025 7:40 am
Getting the old bushing out must have been interesting...?
20 Jun 2025 7:41 am
I actually checked into one. They are out there, mainly in community colleges. BUT, and this is a big but, they won't let you just take something like Machining 101. You have to take some "safety" courses first. Ugh! I guess I can put up with some safety **** to get to the meaty courses. If you want "in" on the machining classes, it has to be part of a degreed program. No more "take my money and teach me ****".ROG62 » 19 Jun 2025, 2:25 pm » wrote: ↑ I wonder how many of them are even around anymore as it seems more and more schools are dropping their classes...
20 Jun 2025 7:51 am
Skans » 20 Jun 2025, 7:37 am » wrote: ↑ I love Casey's bluing paste. I've gotten some excellent finishes using that stuff, of course the polishing is the key. Corrosion resistance of chemical bluing is actually much better than reported on gun forums by "purists" who only trust hot bluing/salts process.
Well, you're way ahead of me. At least you can give it a go. Really, the most difficult thing about the stamped parts is bending them correctly. Rog and I have discussed metal bending. I got one of those small metal benders just to play around with it and see what it is capable of doing. So far, I'm not particularly impressed. It's not precise enough. And, I can't find a bender that is designed to make precision bends. I just don't think one exists.
All of those pivot points and rivet locations are hyper critical.
The bending of the sheet metal needs to be tightly controlled with custom made gauge blocks.
It seems bassackwards but the pieces might need to be bent first, then cut to shape, then sent to a drilling jig .
The gun's original case could be used as the drilling jig.
20 Jun 2025 8:08 am
I was thinking rough-cut the shape of the piece, leaving significant margins for bending/shaping. I also thought it could be milled without bending, but I don't think even an extremely precise mill and good machinist could easily get this right.*GHETTOBLASTER » 20 Jun 2025, 7:51 am » wrote: ↑ All of those pivot points and rivet locations are hyper critical.
The bending of the sheet metal needs to be tightly controlled with custom made gauge blocks.
It seems bassackwards but the pieces might need to be bent first, then cut to shape, then sent to a drilling jig .
The gun's original case could be used as the drilling jig.
20 Jun 2025 8:33 am
It looks like those sheet metal pieces are about 1/16" thick.. milled steel or aluminum would get pretty brittle whittled down that thin.Skans » 20 Jun 2025, 8:08 am » wrote: ↑ I was thinking rough-cut the shape of the piece, leaving significant margins for bending/shaping. I also thought it could be milled without bending, but I don't think even an extremely precise mill and good machinist could easily get this right.
20 Jun 2025 10:01 am
It's been a number of years, but I believe I ended up taking a triangular file and carefully cut a groove in it or it just fell out...*GHETTOBLASTER » 20 Jun 2025, 7:40 am » wrote: ↑ Getting the old bushing out must have been interesting...?

I'll go with the file schtick as it sounds more impressive...
JuCo 5 percenter...72
“Show me the man and I’ll find you the crime” ~ LAVRENTIY BERIA
"Try to get past your passionate ignorance and learn to accept what actually happened." ~ brown's unheeded words of wisdom
If gender is not sex, why should a gender claim change what sex you shower with?
"Libruls are often fascists on vacation..."
20 Jun 2025 10:24 am
Safety s/b integrated into the curriculum, rather than additional classes...trade schools have latched onto the "prerequisite" bs to make it seem important and of course, to garner more monies justifying their existence...Skans » 20 Jun 2025, 7:41 am » wrote: ↑ I actually checked into one. They are out there, mainly in community colleges. BUT, and this is a big but, they won't let you just take something like Machining 101. You have to take some "safety" courses first. Ugh! I guess I can put up with some safety **** to get to the meaty courses. If you want "in" on the machining classes, it has to be part of a degreed program. No more "take my money and teach me ****".
JuCo 5 percenter...72
“Show me the man and I’ll find you the crime” ~ LAVRENTIY BERIA
"Try to get past your passionate ignorance and learn to accept what actually happened." ~ brown's unheeded words of wisdom
If gender is not sex, why should a gender claim change what sex you shower with?
"Libruls are often fascists on vacation..."
20 Jun 2025 10:59 am
I tthink slitting the bushing and peeling it out sounds good.ROG62 » 20 Jun 2025, 10:01 am » wrote: ↑ It's been a number of years, but I believe I ended up taking a triangular file and carefully cut a groove in it or it just fell out...
I'll go with the file schtick as it sounds more impressive...
It is amazing what heat will do though.
That's the way to sleeve an aluminum engine block.
20 Jun 2025 11:05 am
I am convinced that all education and anything healthcare is a scam.ROG62 » 20 Jun 2025, 10:24 am » wrote: ↑ Safety s/b integrated into the curriculum, rather than additional classes...trade schools have latched onto the "prerequisite" bs to make it seem important and of course, to garner more monies justifying their existence...

20 Jun 2025 12:41 pm

ROG62 » 19 Jun 2025, 7:47 am » wrote: ↑ My wife has had horses for like ever...met quite a few farriers over the years...hot, cold, ornery, you name it...guaranteed to make you old before your time... I bet you meet a lot of interesting people though...
I did.
20 Jun 2025 3:29 pm
Agreed...Skans » 20 Jun 2025, 11:05 am » wrote: ↑ I am convinced that all education and anything healthcare is a scam.
JuCo 5 percenter...72
“Show me the man and I’ll find you the crime” ~ LAVRENTIY BERIA
"Try to get past your passionate ignorance and learn to accept what actually happened." ~ brown's unheeded words of wisdom
If gender is not sex, why should a gender claim change what sex you shower with?
"Libruls are often fascists on vacation..."
20 Jun 2025 4:31 pm
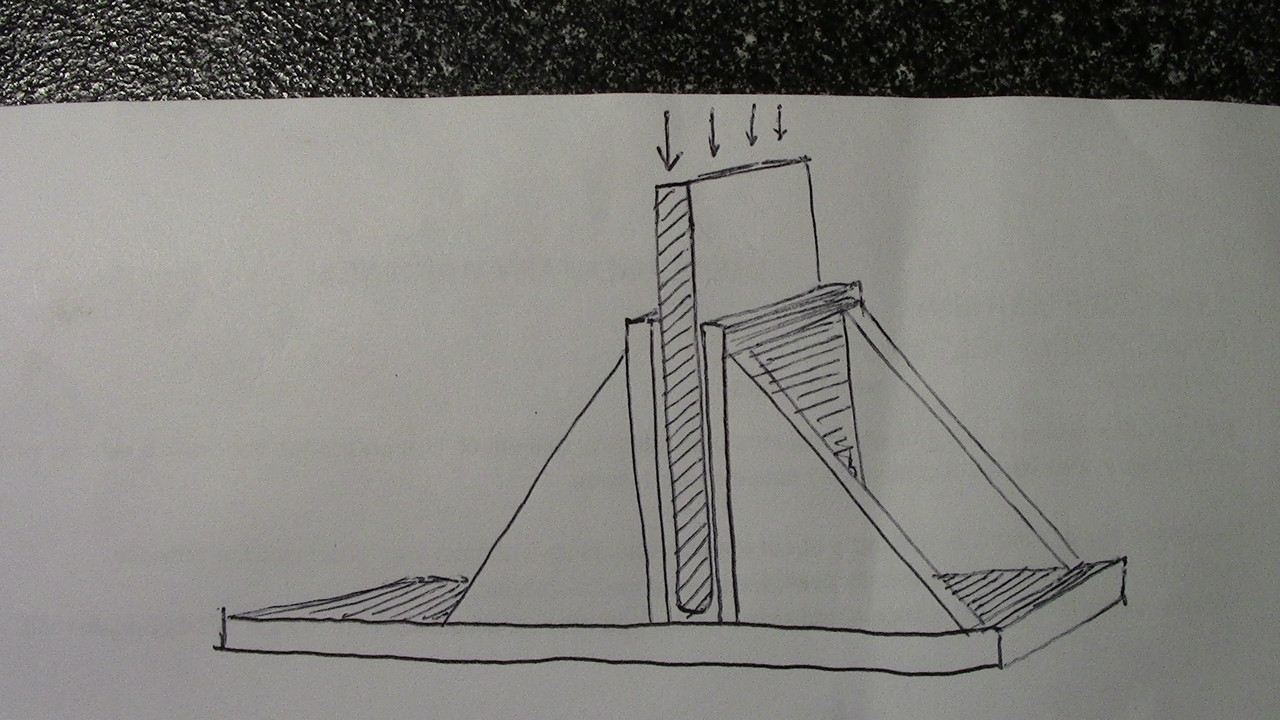
You need to make a fairly massive, U shaped "bending die" out of welded together steel plates.Skans » 20 Jun 2025, 7:37 am » wrote: ↑ I love Casey's bluing paste. I've gotten some excellent finishes using that stuff, of course the polishing is the key. Corrosion resistance of chemical bluing is actually much better than reported on gun forums by "purists" who only trust hot bluing/salts process.
Well, you're way ahead of me. At least you can give it a go. Really, the most difficult thing about the stamped parts is bending them correctly. Rog and I have discussed metal bending. I got one of those small metal benders just to play around with it and see what it is capable of doing. So far, I'm not particularly impressed. It's not precise enough. And, I can't find a bender that is designed to make precision bends. I just don't think one exists.
Let's say you have 1/16" thick sheet metal to form into a U
Let's say this U must have a 1/4" air gap between the 2 sides.
This means your die needs to measure 3/8" between it's sides.
You will also need a 1/4" thick steel plate to use as the tool to force your sheet metal part to be formed perfectly tight inside the die.
Of course your sheet metal gun part needs to be pre bent well enough to be placed into the bending die
I would use lots of axle grease and a hydraulic press to press the 1/4" thick plate down into the bending die.
The steel plates need to be very smooth and fit just snug enough for the folded sheet metal to be a slip in fit.
20 Jun 2025 4:53 pm
Had to bend 1/4 inch 48"L 6063 Channel to a special C shape. Nominally 4 x 8 channel. Two pieces within tolerance.*GHETTOBLASTER » 20 Jun 2025, 4:31 pm » wrote: ↑ You need to make a fairly massive, U shaped "bending die" out of welded together steel plates.
Let's say you have 1/16" thick sheet metal to form into a U
Let's say this U must have a 1/4" air gap between the 2 sides.
This means your die needs to measure 3/8" between it's sides.
You will also need a 1/4" thick steel plate to use as the tool to force your sheet metal part to be formed perfectly tight inside the die.
Of course your sheet metal gun part needs to be pre bent well enough to be placed into the bending die
I would use lots of axle grease and a hydraulic press to press the 1/4" thick plate down into the bending die.
The steel plates need to be very smooth and fit just snug enough for the folded sheet metal to be a slip in fit.
It took us quite awhile.
DUMP THE TRUMP SLUMP 2026!
Bump Caps Recommended..
Bump Caps Recommended..
Who is online
In total there are 2560 users online :: 3 registered, 12 bots, and 2545 guests
Bots: DuckDuckGo, AHC/2.1, MicroMessenger, proximic, ADmantX, CriteoBot, Mediapartners-Google, facebookexternalhit, Googlebot, Applebot, curl/7, bingbot